Last modified: 2026-11-08 20:59:10
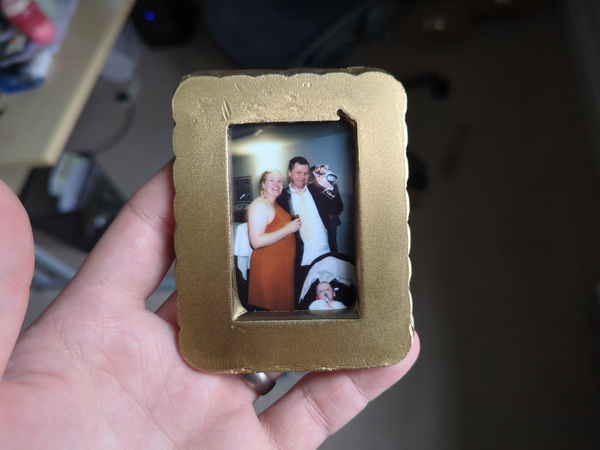
< 2026-11-07 2026-11-09 >Picture frame:
Obviously pretty terrible, but do I now have enough to write a blog on how to make a CNC plasma cutter on the cheap with HF start? Probably.
Key points of my design are:
I reckon post it now even though the machine is not quite working properly otherwise it's just going to get longer and more rambling.
https://incoherency.co.uk/blog/stories/cnc-plasma-cutter.html
I realised that I don't need to make an adjustable torch holder, I can just let the slidey part sit on top of its guides instead of sliding in between them:
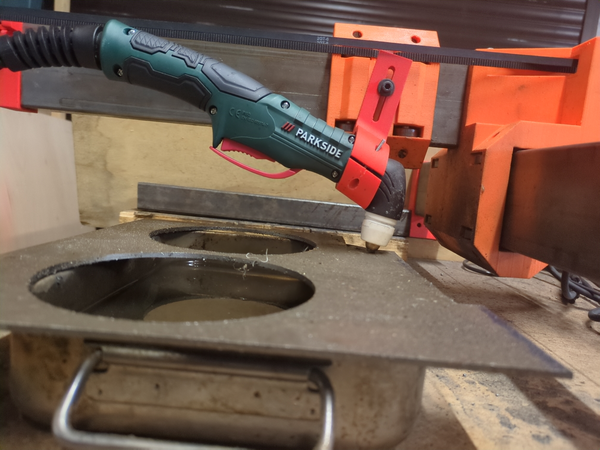
This way the torch clamp angle is already adjustable.
And indeed tilting it like that is a big improvement to the bevel but not much improvement to performance. I cut out another heart from 3mm steel at 500 mm/min and it went fine but again lots of slag on the bottom, but not much bevel. And the arc is visibly lagging based on the marks around the edge.
I tried to do one at 650 mm/min and it didn't cut all the way through.
Also, ChatGPT's worries about the wooden bench being a fire risk are ill-founded, a much greater threat to the bench is the water tray. The compressed air shoots loads of water out of the tray and on to the bench and it has now soaked into the MDF top and lifted it up in places so the bench top is now nowhere near flat, annoying.
I did experiment with lower pressure as suggested by some YouTube comments but that was predictably unhelpful, it made it worse.
From reading up online I found that some people report turning a potentiometer inside the machine to increase the cutting power, so I opened the machine up to have a look.
I found that the circuit boards were labelled "UNICUT45", is this a 45 amp machine with the power turned down to 30 amps? I didn't know which way to turn the potentiometer so I tried cutting with it all the way one way and then all the way the other. Turning it all the way anticlockwise seems to make it more powerful! So this is good. I don't know if it will impact longevity but that's a problem for the future.
I cut a heart out of 3mm steel at 1000 mm/min! This is definitely a big improvement, I had previously failed to cut all the way through at 650 mm/min. My previous best success was at 500 mm/min earlier today.
Here's a comparison (erroneously the 500 mm/min one is labelled "650"), unfortunately I had chipped off the bottom slag on both but I could tell visually that there was a lot less bottom-side slag on the 1000 mm/min one.
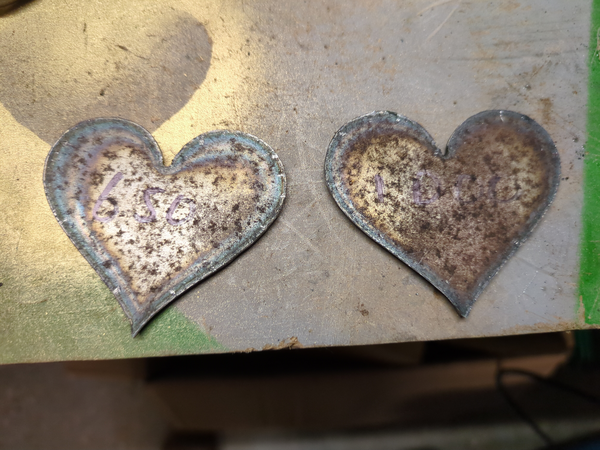
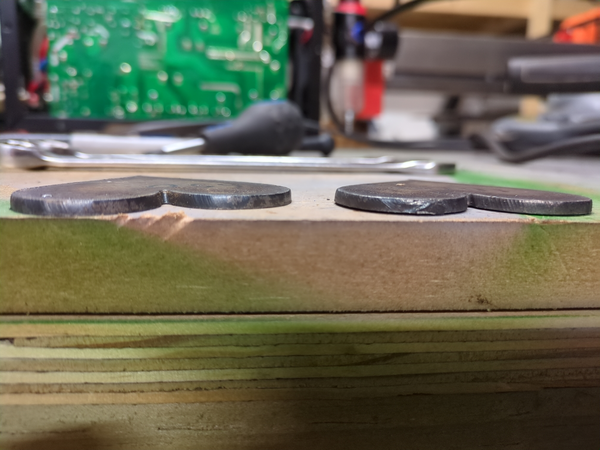
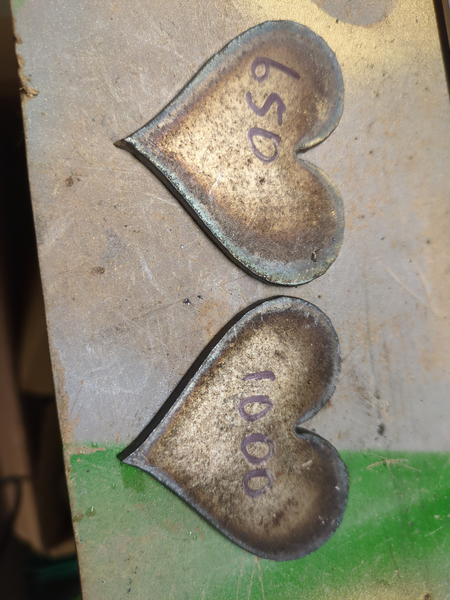
So the 1000 mm/min one has less slag on top, a lot less slag on bottom, slightly rougher edges, similar amount of arc lag, but had some places where it hadn't cut all the way through. The 500 mm/min one from earlier had cleaner cut edges, but worse slag, but cut all the way through.
So probably I could slow down from 1000 mm/min and get an improvement on both. So this is looking quite promising actually.
I moved on to messing about with the 5mm steel again. I made a bunch of test cuts in straight lines on the side of the sheet and determined that 500 mm/min seemed cleanest even though it didn't quite penetrate reliably.
Top side:
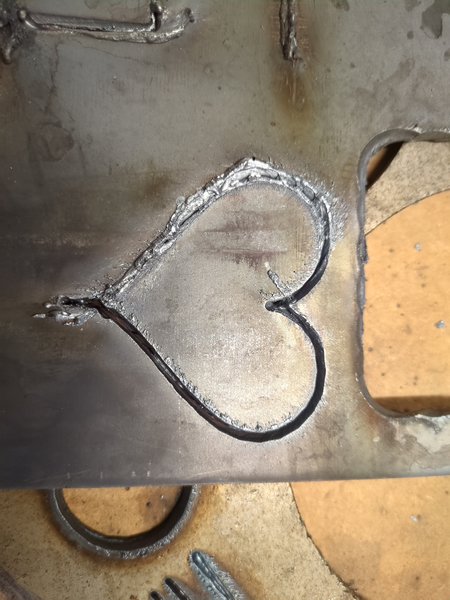
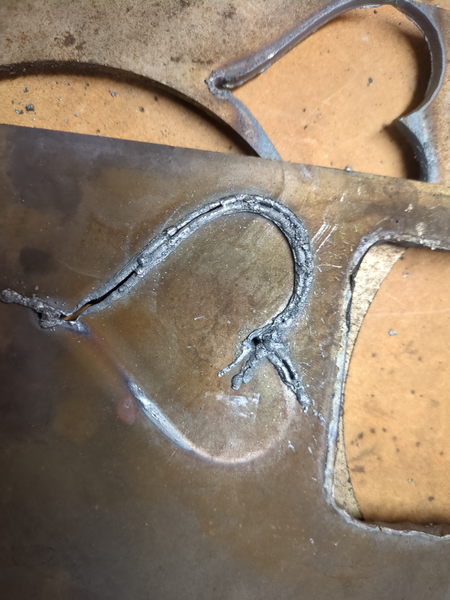
So the best part on this is the very last bit that was cut, which has the least slag on both sides. At the start it hasn't penetrated all the way through and left a lot of slag on the top side, and for the second half it did go all the way through but left a lot of slag on the bottom side.
So this is very interesting, shows that even at constant current and feed rate and torch height the cut quality can vary quite a lot.
I think the only explanations for this are:
I think I recall that the compressor kicked on for the second half of this cut and that is the bit that cut better, which does make it look like less pressure makes it work better. But it could just as easily be that the second half of the cut had a more optimal effective torch height.
I think we are getting somewhere though. I am keen to install the new consumables and see if they help, if all of the difficulty is caused by the nozzle orifice being off axis or something (consistent with needing to tilt it to a funny angle to get a straight cut) then this machine might just instantly start working better with a new nozzle. Probably wishful thinking. More likely that the torch has the mountings eccentric and no consumables will fix it.
But almost cutting through the 5mm plate at 500 mm/min is a big improvement over having to reduce to 200 mm/min like I did for the picture frame.
So today's improvements have come from:
A good thing to try would be running a bunch of long-ish line cuts at different pressure regulator settings.
Would be good to measure the cutting current using a DC clamp meter but I don't have one.
< 2026-11-07 2026-11-09 >